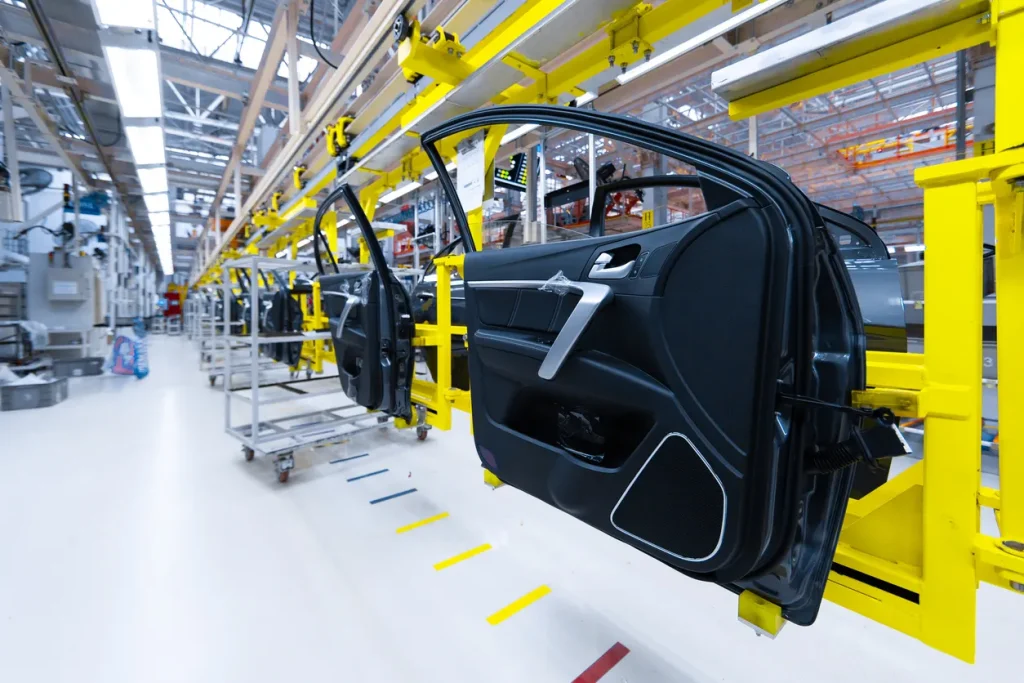
An automotive component reaches an inspection station having already been through several processes designed to make it look expensive. Paint adds gloss. Grain adds texture. Forming adds curvature. Each one is a problem for an optical sensor, because a sensor that reads a flat sample on a bench will not read that same color the same way once it is curved, grained, and clear-coated.
EMX builds optical sensors in Cleveland for these lines, and the specification that decides an automotive application is usually a property of the part rather than a number on a data sheet. Four properties account for most of the difficulty. Each one rules some sensors in and rules others out well before line speed or output type enters the conversation.
Work through these against the actual component before comparing models.
Finish varies across a single part. A door panel can carry a soft-touch surface, a grained insert, and a gloss bezel in one molded color. Light returns differently from each, so a single taught reference will not cover the part.
The surface curves and the standoff moves. Fixturing and robot presentation both vary distance and angle, and any sensor whose reading depends on standoff will report that variation as a process fault.
The mark shares a hue family with its background. Date codes and witness marks on automotive components are frequently printed dark on dark or applied color on color.
The material is invisible. Adhesive beads, sealant, bearing grease, and UV-readable codes all have to be verified and none are visible under plant lighting.
Pro Tip: Teach a color check against the real spread of acceptable production, not one golden part. A band taught from a single sample is almost always too tight, and the operator’s response to a line generating false rejects is to widen it until it stops catching anything at all.
The ColorMax-1000 reports color and luminosity together, which lets one sensor family handle a matte insert and a gloss bezel without confusing brightness for hue. It holds up to 15 taught colors, outputs analog RGB at 10-bit resolution, switches at 20 kHz, and works up to 150 mm from the target with 4 mm, 8 mm, and 25 mm spot sizes.
Two adjustments carry the application. Spot size has to fit inside the smallest feature being checked, because a spot larger than the target reads background along with it. White balance corrects several sensors running the same check on different machines, so their readings agree instead of drifting apart station by station.
Where this breaks down: the target is translucent. Reflected color sensing needs an opaque surface, so tinted films, lenses, and glazing want transmitted measurement instead. The ColorMax VIEW is built for that, resolving color variation to 0.5% at 20 kHz with an operating range up to 500 mm.
When a check only has to confirm a mark or feature is present, contrast sensing tolerates that geometry better than color sensing, because it grades against the local background rather than an absolute reference. The CNTX contrast sensor reads 50 grayscale levels on a numerical display, with a 3 mm standard spot and a 0.4 mm option for dense layouts, and its broad-spectrum source means the mark’s color barely matters.
Where this breaks down: the mark and the background land at the same brightness in different hues. Contrast sensing needs a contrast to grade. A dark blue code on a black substrate reads as one surface to the CNTX, and that is a color measurement.
The CMYX color mark sensor takes the case the CNTX cannot. It switches at 40 kHz against the ColorMax line’s 20 kHz and resolves marks down to 0.5 mm, holding a small color-on-color mark at speeds where a slower sensor is still integrating once the mark has passed.
Where this breaks down: the mark is large and clearly darker or lighter than what surrounds it. That job belongs to the CNTX, and specifying color mark detection for it buys resolution the application will never call on.
The UVX luminescence sensor verifies materials that fluoresce under ultraviolet light: adhesives, epoxies, sealants, greases, UV inks, and optical brighteners. A 370 nm UV LED rated for 100,000 hours drives it, sensing to 700 mm with a 6 to 8 mm spot at 50 mm and three selectable source intensities. Relative signal reads 00 to 99 on the display, and both a discrete PNP/NPN output and a 0 to 5V analog output are available at once, so a bead can be checked for presence on one output and for quantity on the other.
Where this breaks down: in two separate ways. If the material carries no luminescent component, this is the wrong physics and gain will not rescue it, so confirming the tracer with the adhesive supplier is a first step rather than a last one. Separately, the housing is IP65, rated against dust and low-pressure water but explicitly not for pressure washdown, which rules it out of a station hosed between shifts unless it is enclosed. EMX also states the UVX is not intended for personal safety applications.
Dive Deeper: Browse EMX’s color sensor applications for how these checks run on production lines.
Everything above narrows a catalog to a short list. One production component settles it, because gloss, grain, curvature, and batch spread move the numbers in ways no data sheet predicts.
That is what free sample testing is for, and it is the strongest thing EMX offers on this side of the business. Ship the actual part, and EMX’s engineers run the candidate sensors against it and report what each read, at what setting, and what the mounting will need to hold. Send in the component giving you trouble and let the readings pick the sensor. If output types or fixturing are the open question, our team will take the application.